The 5 thermoforming mistakes I keep finding
Plants all over the world, the same five thermoforming mistakes. Most of them were built in before the first cycle, and nobody checks them later. Here they are, explained simply, with what you can check yourself tomorrow morning.
Hard air.
Every mistake below forces you to run the sheet hotter. Hot sheet sags, outer and inner cavities run differently, and your process window gets small. Fix the five points, and you can run cooler, faster and more stable.
Mistake 1No preheater – or the wrong one
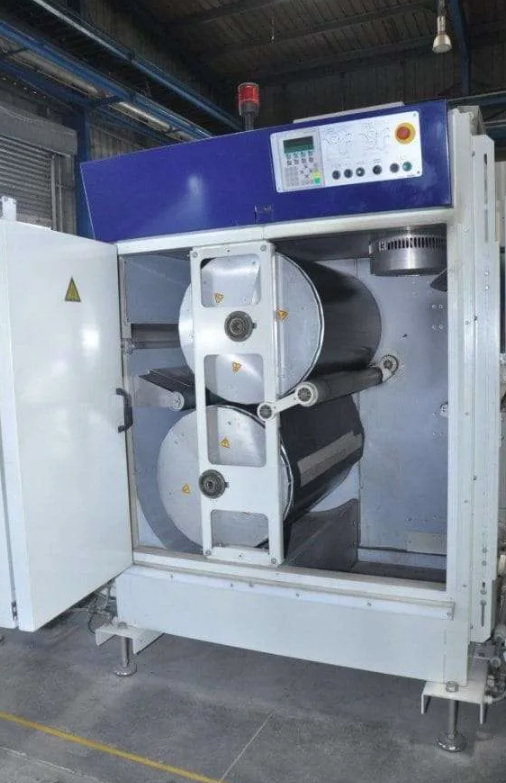
Think of a frozen pizza. A hair dryer warms the top, but the middle stays cold. Put it on a hot pan, and the heat goes straight in. Plastic sheet works the same way. A roll preheater touches the sheet, so the heat reaches the core, evenly. This matters most with PP.
What I see in plants
Preheaters where the sheet runs in loops through hot air. That is a hair dryer. It does very little.
Suppliers who don't sell preheaters will tell you that you don't need one. At low speed you hardly see a difference. At high cycle rates the heating time gets short, and that is where contact heat counts. This is why some machine builders offer 2-roll and 4-roll units.
The preheater itself must be well insulated, so the heat cannot escape and goes straight into the sheet. I still find preheaters without insulation – they don't help either.
Run the rolls as hot as possible without the sheet sticking or melting. It takes time to heat the core of the sheet.
Check it yourself
- Does your preheater touch the sheet? If not, ask why.
- Running inline? Place calender and haul-off as close to the thermoformer as you can. The sheet should enter the machine as warm as possible.
Mistake 2Forming air pressure too low
Press play dough into a mould. Press hard, and even firm dough fills every corner. Press softly, and you have to make the dough softer and softer, until it sags and gets messy. Low air pressure does the same to your sheet.
What I see in plants
Minimum forming air pressure in the cavity: 6 bar. Better: 8 bar. This goes for PS, PET, PP and other materials.
Below 6 bar you have to make up for it with sheet temperature. Hot sheet sags more, outer and inner cavities run differently, and the hot sheet slides differently on the plug. The goal is the opposite: high air pressure, low sheet temperature.
Check it yourself
- Do you enter the forming pressure on a screen? Then your machine has a proportional valve.
- Most of these valves need 10 bar supply pressure. With less, the valve never opens fully. The display shows 8 bar, the cavity never gets it.
- Ask your machine supplier. Some offer a small booster compressor for the valve.
- These valves are also fragile. Many plants replace them with a classic manual pressure regulator.
Mistake 3The air arrives too slowly in the cavity
Try to blow up a balloon through a thin drinking straw. You blow hard, but it takes forever. Through a thick tube it fills at once. Forming air has to hit the cavity like an explosion. If there is a "straw" inside your tool, you have to make the sheet hotter to make up for it.
What I see in plants
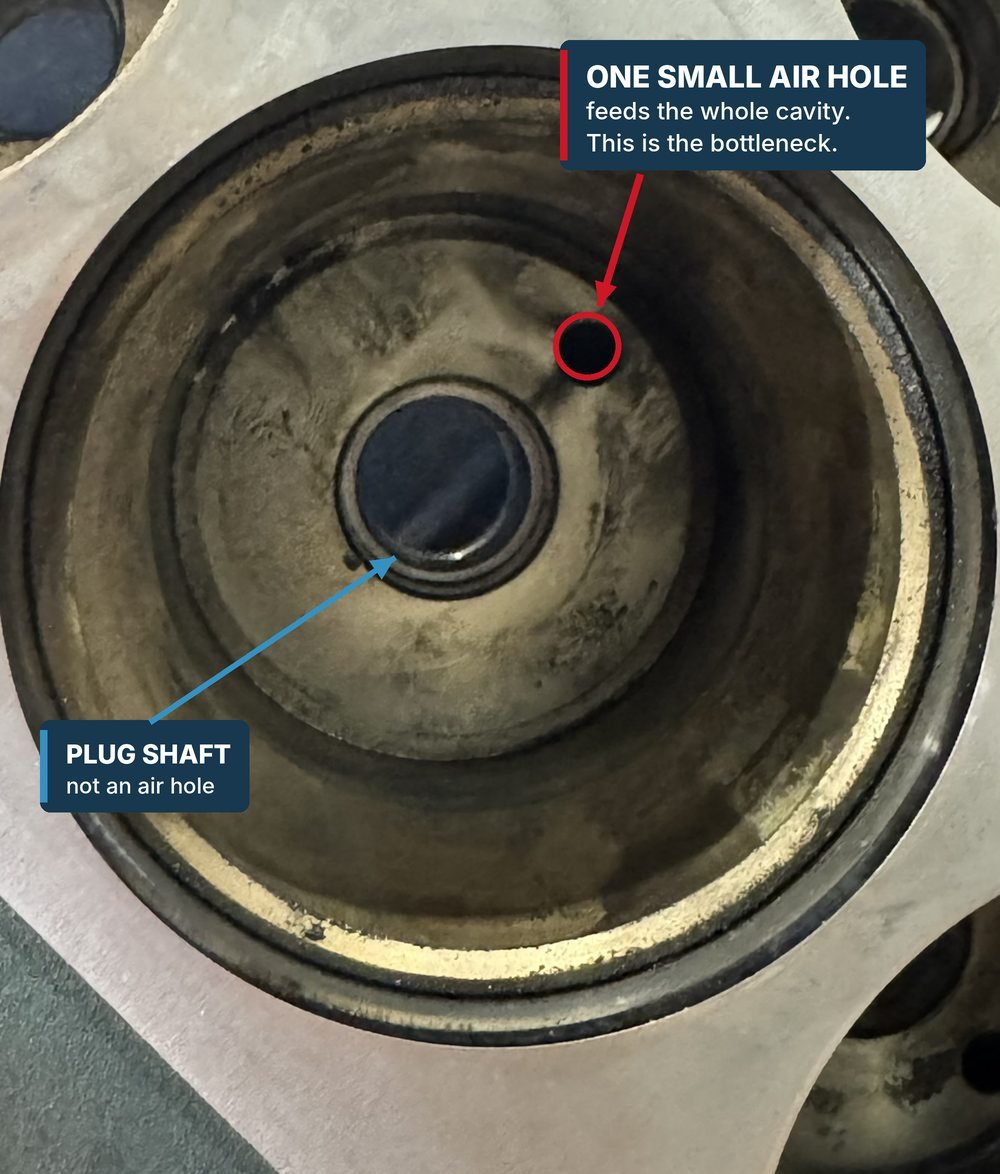
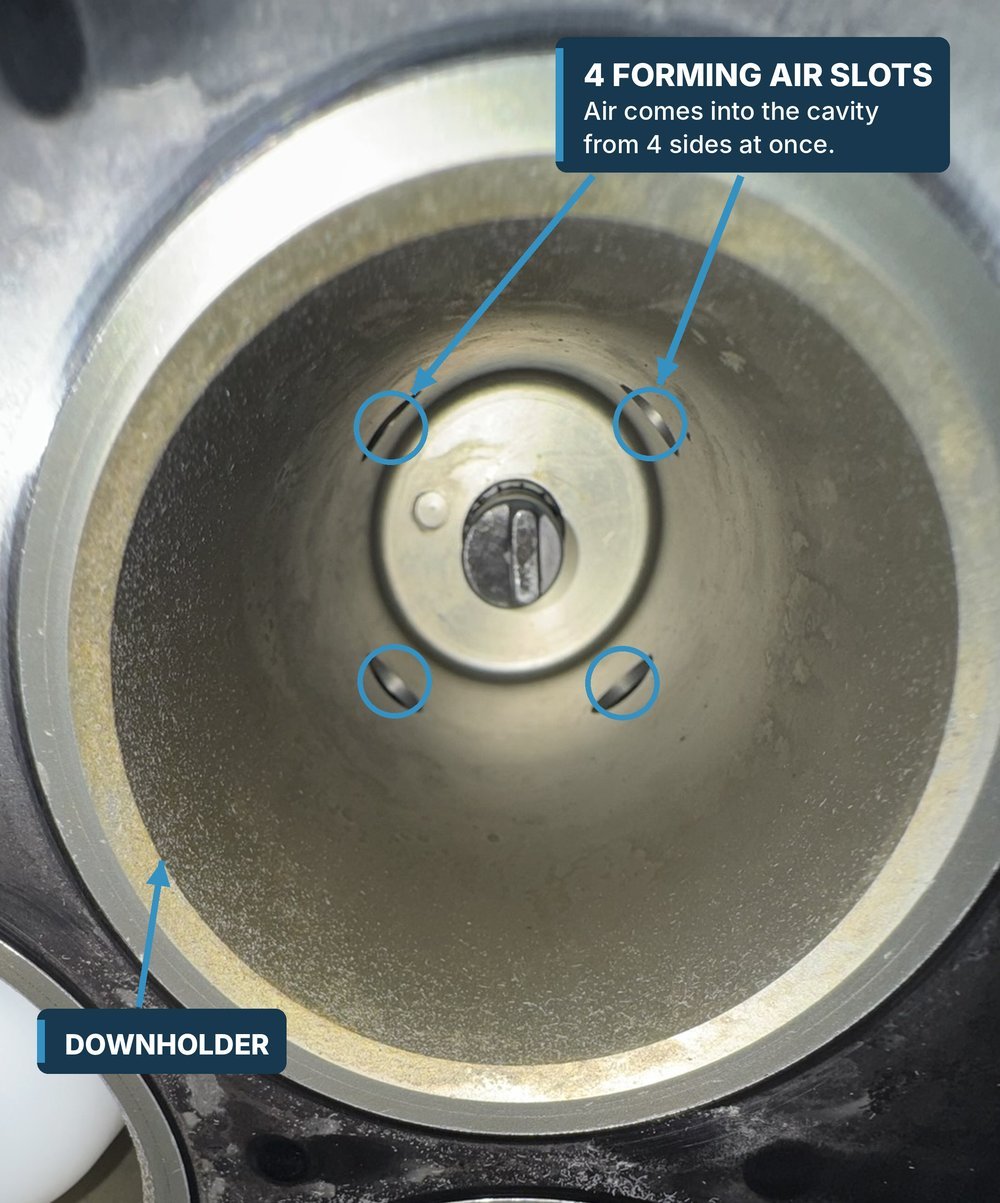
The pressure in the tank is fine. But on the way into the cavity, the air gets stuck. In many tools I found the bottleneck in the upper mould: one small bore feeding the downholder, and with it the whole cavity.
Check it yourself
- Fit a pressure gauge in the upper tool, where the toolmaker drilled the forming air bores. Compare it with the gauge on the tank. Any difference means: go looking.
- Take out one downholder. How many bores feed the air to it, and how big are they?
- One small bore in front of the downholder usually doesn't work. Check if the bores can be made bigger, or if a new block with a fast air supply makes sense.
Mistake 4The forming air tank is too small
Fill a bathtub with a small cup. After every cup you walk back to the tap and wait. A small air tank is that cup. At high speed it can't refill in time, and the pressure you set is never reached.
What I see in plants
Many thermoforming machines come with a 50-litre forming air tank. If you are lucky, 2 × 50 litres. With bigger tools and large-volume products, the machine simply runs out of air.
On larger tilt-mould machines I recommend at least 2 × 200 litres.
Check it yourself
- Put a pressure gauge on the tank.
- Watch it while you increase the cycle rate. Does the needle come back up before the next shot?
- If not, the pressure you set is no longer the pressure you form with.
Mistake 5Plugs with a too big radius
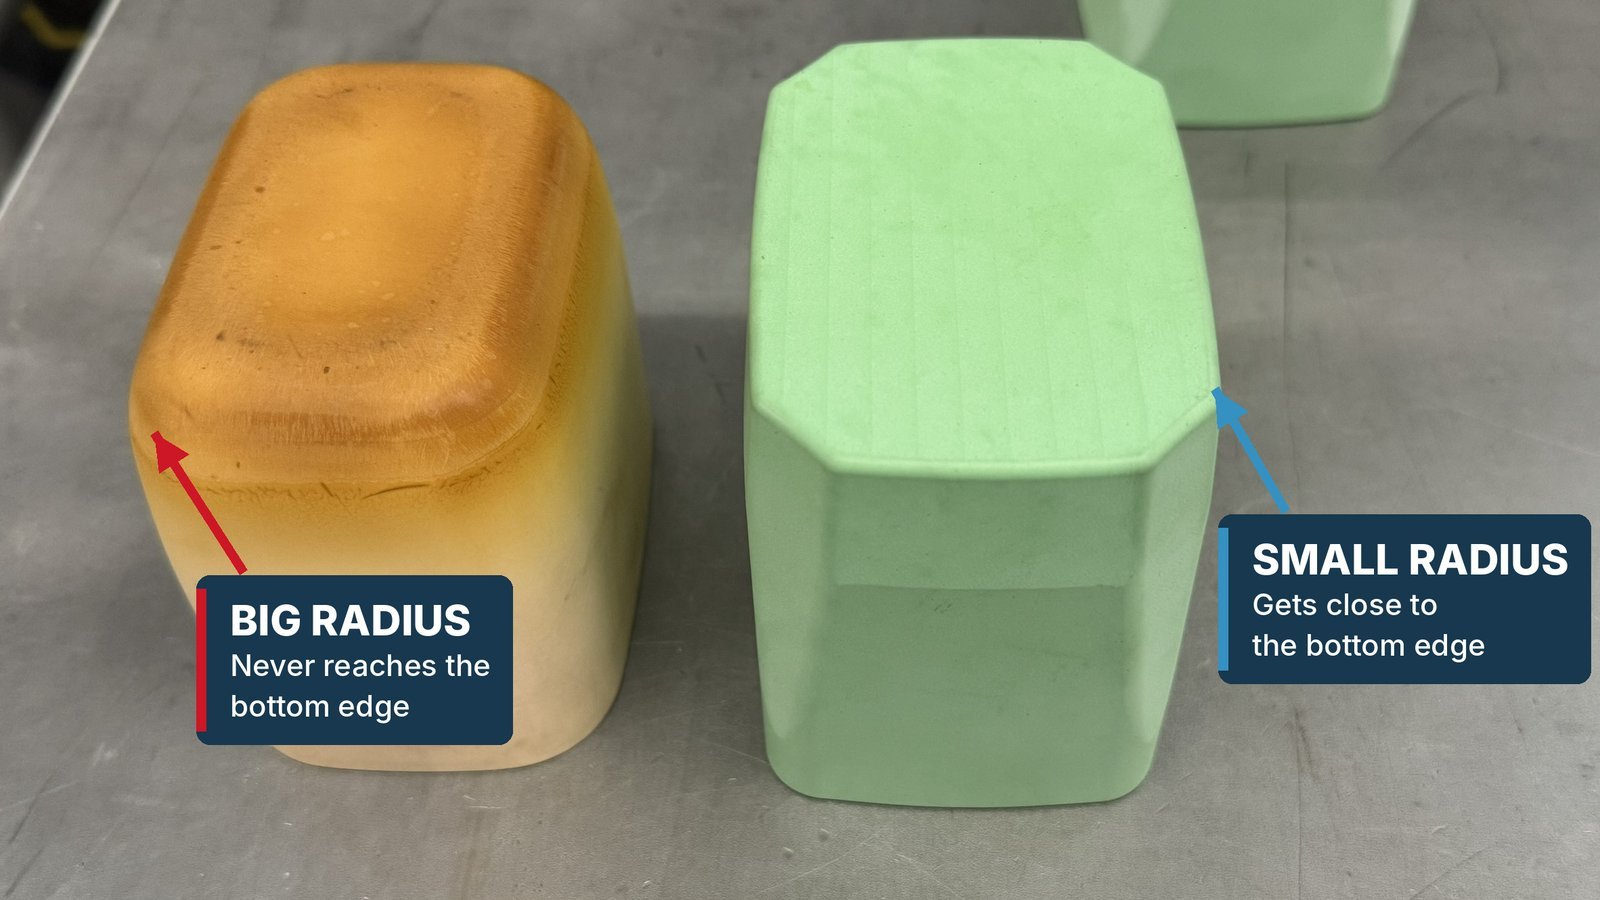
Push a sheet into a cup with a tennis ball. You never reach the corner at the bottom. With a block that has only slightly rounded edges, you get right into the corner.
What I see in plants
Most plugs have a big radius. That tells me the process was designed for hot sheet and low air pressure.
With a big radius the plug stays far away from the bottom edge of the cup. The edge comes out soft and not well defined.
What to do
- First fix mistakes 1 to 4: run cooler sheet with high forming air pressure.
- Then you can use a plug with a smaller radius. It gets closer to the bottom edge: more definition, more stable cups.
- More on plug geometry: Plug assist design for thermoforming cups.
Thermoforming mistakes: quick answers
What forming air pressure do I need in thermoforming?
At least 6 bar in the cavity, better 8 bar – for PS, PET, PP and other materials. Below 6 bar you have to run the sheet hotter to fill the mould, and the process becomes unstable.
Why does my machine not reach the forming air pressure I set?
Most proportional pressure valves need about 10 bar supply pressure. With less, the valve never opens fully: the display shows the set value, the cavity never gets it. A forming air tank that is too small for your tool and cycle rate has the same effect.
Do I need a preheater for PP?
For PP at higher cycle rates: yes, a contact roll preheater. It brings the heat into the core of the sheet. Hot-air preheaters and preheaters without insulation do very little. Running inline, place the extruder calender as close to the thermoformer as possible.
How big should the forming air tank be?
Many machines come with 50 litres. On larger tilt-mould machines I recommend at least 2 × 200 litres. Check with a gauge on the tank: the needle must come back up before the next shot.
Why is the bottom edge of my cups soft and not defined?
Often the plug radius is too big, so the plug stays far away from the bottom edge. With cooler sheet and high forming air pressure you can use a plug with a smaller radius that gets closer to the edge.
Read more on avoiding thermoforming mistakes
This list could go on.
Most plants I visit have at least two of these five, and nobody notices, because the machine "runs". Send me a photo of your upper tool and your forming air settings. I'll tell you where I would look first. No cost, no strings.